Machining Thin-Wall Aluminum Parts Without Warping
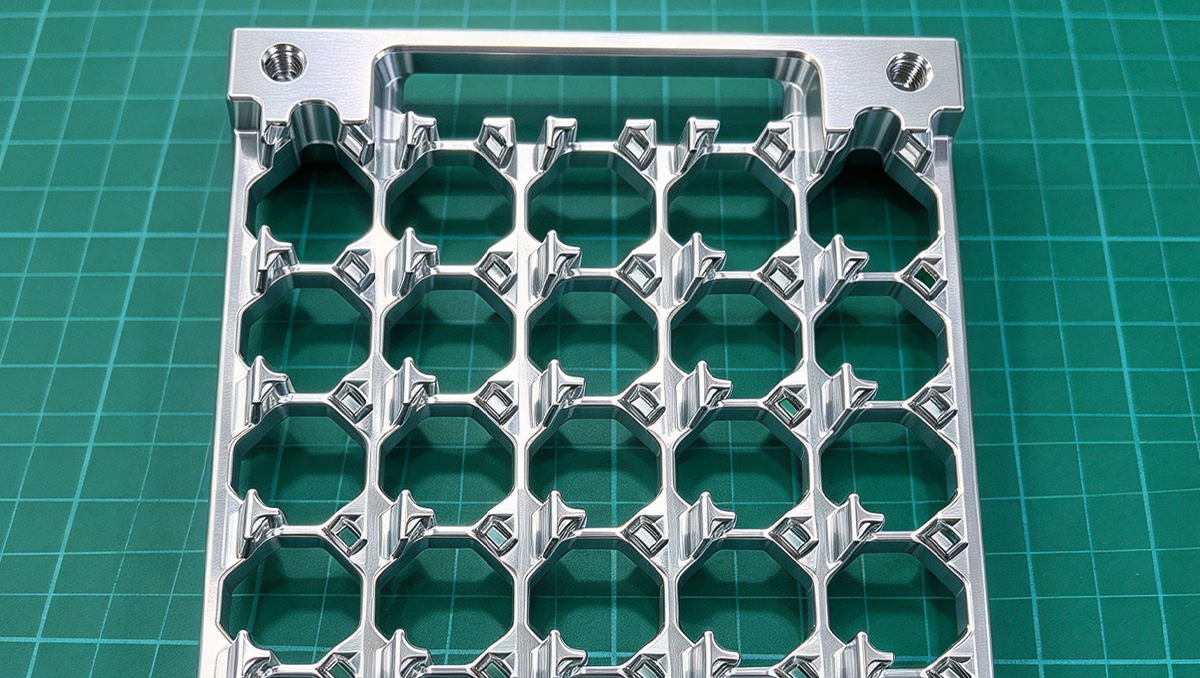
Thin-wall aluminum parts, especially hollowed-out ones, tend to move during machining. Cut them to size and they come off the machine bowed or twisted, because the thin walls can’t hold their shape against the stress in the metal. The fix isn’t a clever cut, it’s the order you work in. Here’s the process we use on a one-off thin-wall part.
Why they move
Two kinds of stress cause it: stress already locked into the raw plate, and stress the machining adds through cutting force and heat. In a solid block that stress is balanced and hidden. As you cut material away, and a hollow part means a lot of it, the balance breaks and the part moves. A thick part is stiff enough to resist; a thin wall isn’t, so it bows or twists.
1: Rough out, leave 1 mm
We rough the shape but don’t go to size. Every dimension is left with 1 mm of stock. That takes most of the material off, which lets the locked-in stress release, and it leaves enough skin to clean the part back true after it moves. Machining straight to size here would leave the part out of tolerance with nothing left to fix it.
2: Stress relief
With the part roughed out, we relieve the machining stress before the final cuts, in two stages:
- Oven: 180°C for 4 hours.
- Then room temperature for 50 hours.
The heat lets the residual stress relax; the time afterward lets the part settle. By the end it has done its moving, while it still has the 1 mm to spare.
3: Finish with light cuts
Once it’s stable, the part goes back on the machine and is finished to size with light cuts off that 1 mm. Small depths of cut keep force and heat low, so finishing doesn’t add fresh stress. With the stress already out, what you cut is what you keep.
A few things that help
- Sharp tools and light finishing passes.
- Take material off evenly, not one side at a time, so the part stays balanced.
- Support the part without clamping hard on the thin walls. Heavy clamping bends them, and the bend shows once you release it.
Custom thin-wall machining
Thin-wall and hollowed-out parts are among the hardest to hold to tolerance, and getting them right is mostly process and patience. We machine thin-wall aluminum parts as one-offs and small runs, with stress relief built in where the part needs it.
Send us your drawing or a sample with the material and tolerances you need. We’ll work out the process to keep it in spec and confirm the details before we start.
Share this article

Written by : Alex
A quick overview of the topics covered in this article.
Latest articles
October 18, 2026
September 15, 2026
September 9, 2026